Product Overview
SinoDiam CBN-B10 Black Friable Cubic Boron Nitride is a synthetic CBN abrasive grit positioned for manufacturers of resin-bond grinding wheels and precision grinding tools used on suitable hardened ferrous materials.
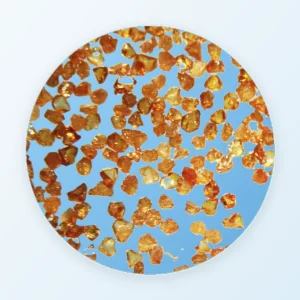
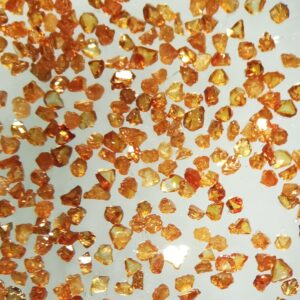
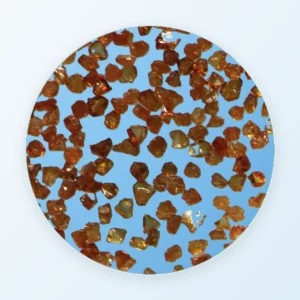
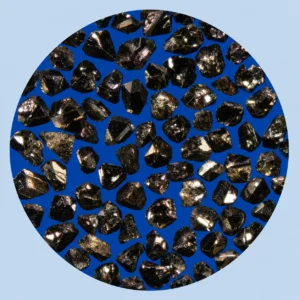
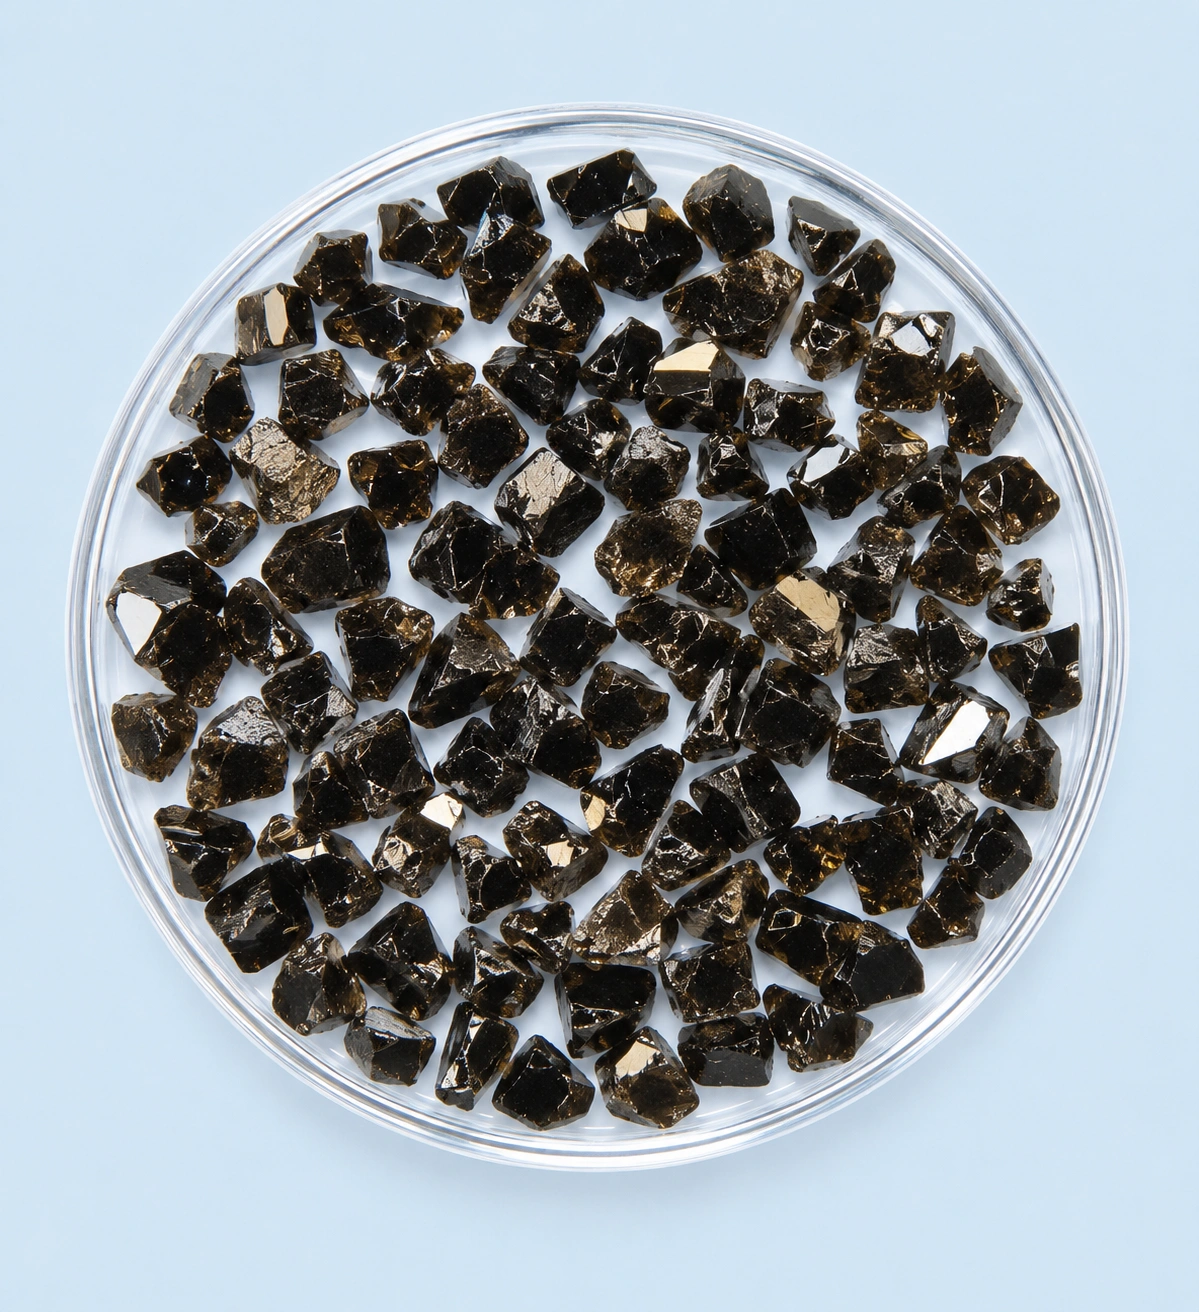
CBN-B10 is characterized in the SinoDiam product catalogue by its black appearance, irregular crystal morphology, friable structure and low-toughness grade positioning. These characteristics make it a candidate for resin-bond applications where controlled particle fracture and cutting-edge renewal are important selection considerations.
Friability describes the tendency of abrasive grains to fracture under applied mechanical conditions. In a suitable grinding wheel, controlled fracture may expose new cutting edges as the original abrasive points wear. However, excessive grain breakdown can cause premature grain loss, increased wheel consumption or reduced grinding efficiency.
CBN-B10 should therefore be evaluated as part of a complete grinding system involving crystal friability, resin-bond retention, abrasive concentration, wheel structure, grinding load and workpiece characteristics.
Cubic boron nitride is widely used in grinding many hardened steels and other suitable ferrous alloys. Compared with diamond, CBN generally offers more favorable chemical behavior in many steel-grinding applications. The actual material selection depends on workpiece composition, heat treatment, operating temperature and grinding conditions.
CBN-B10 is especially relevant to fine and precision grinding applications where wheel designers wish to evaluate the relationship between abrasive fracture and effective cutting-edge exposure. The correct balance cannot be determined solely from the grain’s black color or low-toughness designation.
Potential workpieces include selected hardened tool steels, alloy steels, high-speed steel components and precision ferrous-metal parts. Workpiece hardness, grinding allowance, heat treatment, coolant, wheel dressing and surface-integrity requirements should all be considered.
The historical SinoDiam catalogue references 50/60 through 325/400 mesh CBN-B10 abrasive. Fine grinding discussions may emphasize intermediate and finer fractions, but current availability, grading limits and the appropriate mesh size must be confirmed for each application.
For technical selection or quotation, please provide the required CBN mesh fraction, resin type, finished-wheel configuration, workpiece material and hardness, grinding conditions, estimated order quantity and delivery destination.
Technical Specifications
CBN-B10
Black Friable Cubic Boron Nitride
Synthetic Cubic Boron Nitride (CBN)
SinoDiam
Black
Irregular / Friable
Low — Catalogue Classification
Resin Bond
50/60–325/400 Mesh — Verify
Confirm Current Size List
Request Grade-Specific PSD
Confirm Applicable Mesh Specification
Request Measured Test Data
Verify Representative Particle Morphology
Selected Hardened Steels / Tool Steels
Suitable Alloy Steels / HSS Components
Resin-Bond CBN Grinding Wheels
Confirm Phenolic / Polyimide Suitability
Determine by Wheel Formulation
Determine by Finished Tool & Process
Application-Specific Requirements
Confirm Through Grinding Trials
Request Current Product Specification
Black color, irregular morphology, friability and low-toughness positioning reflect the historical SinoDiam CBN-B10 catalogue description. Current mesh availability, PSD, friability, grain strength and performance require appropriate technical confirmation. No fixed surface roughness, wheel-wear reduction, grinding efficiency improvement or scratch-free result is guaranteed.
Black Friable CBN Crystal Morphology & Grinding Behavior
CBN-B10 is positioned for grinding-wheel systems where abrasive grain fracture and cutting-edge renewal may play an important role. The desired behavior depends on the complete wheel construction and grinding conditions.
Black Irregular CBN Crystals
CBN-B10 is characterized by black, irregular abrasive particles. Actual crystal geometry and particle-size distribution should be evaluated using representative material from the requested grade.
Friable Grain Structure
Friable CBN may fracture under suitable grinding forces. The amount and character of fracture depend on crystal defects, particle size, mechanical loading and wheel retention.
Potential Cutting-Edge Renewal
Controlled fracture can expose fresh abrasive contact points. The resulting cutting behavior must be balanced against possible excessive grain breakdown or premature abrasive release.
Low-Toughness Classification
Low toughness is a relative catalogue classification, not a universal numerical fracture-strength value. Compare actual friability and grinding behavior through appropriate material tests.
Resin Retention & Exposure
Resin chemistry, fillers, abrasive concentration and processing conditions affect how CBN grains are retained and exposed during grinding.
Wheel Wear & Surface Integrity
Excessive wheel wear, grain pull-out or glazing can change grinding behavior. Finished-wheel testing must consider workpiece damage, grinding forces and dressing requirements.
Friable Does Not Mean Automatically Self-Sharpening
A friable CBN grain may expose new cutting points through controlled fracture. However, this effect depends on abrasive size, grinding forces, resin-bond retention and wheel wear. If particles fracture too rapidly, the wheel may lose abrasive material before useful cutting can be maintained. CBN-B10 should be evaluated for the intended balance between grain renewal and wheel durability.
CBN-B10 Resin-Bond Grinding Wheel Compatibility
Resin bond is the primary catalogue application for CBN-B10. A suitable wheel must provide effective abrasive retention while permitting the desired cutting and grain-fracture behavior.
Phenolic Resin-Bond Wheels
CBN-B10 may be evaluated with selected phenolic resin formulations. Review resin chemistry, fillers, curing conditions, abrasive concentration and grinding requirements.
Polyimide Resin-Bond Wheels
Polyimide-based systems may impose different thermal and mechanical requirements. Confirm the compatibility of B10 grain characteristics with the selected bond and manufacturing process.
Abrasive Concentration & Wheel Structure
Wheel porosity, abrasive loading and resin content influence grain support, chip space, coolant access and wear behavior. The correct formulation depends on the grinding duty.
Grain Fracture vs. Bond Release
Fracture within an abrasive grain is different from losing a complete particle from the wheel. Both mechanisms should be distinguished during performance evaluation.
Wheel Curing & Manufacturing
Pressing, curing and subsequent machining steps influence the finished grinding wheel. Validate the process against resin specifications and abrasive characteristics.
Dressing & Grinding Conditions
Wheel conditioning, loading, grinding speed, depth of cut and coolant can affect cutting forces and grain-fracture behavior. A friable grade does not eliminate the need for suitable dressing.
When Should a More Friable CBN Grade Be Evaluated?
Consider a friable abrasive when the grinding system may benefit from controlled cutting-edge renewal. If the process places high mechanical loads on individual grains, a more fracture-resistant grade such as CBN-A20 or CBN-B20 may be a better candidate. This is a selection direction, not a guaranteed substitution rule.
CBN-B10 Mesh Size Selection for Fine & Precision Grinding
The historical SinoDiam catalogue lists CBN-B10 fractions from 50/60 to 325/400 mesh. The examples below describe preliminary size-selection directions for resin-bond grinding-tool development.
50/60 Mesh
Coarser Grinding Evaluation
Consider only where relatively larger particles and friable grain behavior are appropriate. Verify abrasive survival, wheel retention and the intended grinding load.
120/140 Mesh
Intermediate Precision Grinding
Evaluate when a medium-fine grit size is appropriate for the wheel and workpiece. Compare material removal, cutting-point renewal and resin-bond wear.
325/400 Mesh
Fine Grinding Evaluation
Consider where a relatively fine abrasive fraction is required. Oversize control, dressing, wheel structure and surface quality remain critical.
Important Grit-Selection Factors
Mesh Grading & PSD
Establish the grading standard, particle-size distribution and acceptance limits. Nominally identical mesh names may not establish equivalent products.
Friability by Particle Size
Particle-fracture characteristics may differ across grit sizes. Obtain grade-specific friability data or representative test results where necessary.
Wheel Concentration & Structure
Resin content, abrasive concentration and wheel porosity affect grain support and cutting behavior. They should be selected as a complete system.
Grinding Finish & Material Removal
Finished-surface quality depends on grit size, wheel condition, workpiece and process. Fine CBN grit does not independently guarantee a specific Ra value.
Choosing Fine-Grinding CBN Mesh Sizes
The historical CBN-B10 product description emphasizes intermediate and finer grit sizes, including 120/140 through 325/400 mesh, for selected fine-grinding applications. Actual suitability depends on the wheel design and workpiece, and the currently available grit fractions must be confirmed before purchase.
The historical 50/60–325/400 mesh scope is a catalogue reference, not confirmation of current inventory or particle-size tolerances.
Recommended Applications of CBN-B10 Black Friable Grit
CBN-B10 is positioned for selected resin-bond grinding applications involving hardened ferrous materials and precision surface requirements. Each application requires evaluation of wheel formulation and grinding conditions.
Hardened Tool Steel Finishing
Evaluate resin-bond CBN-B10 wheels for selected hardened tool steel workpieces where cutting-edge renewal and finished-surface requirements must be balanced.
Alloy Steel Precision Grinding
Suitable alloy steel components may be ground using resin-bond CBN tools. Assess heat treatment, grinding forces, thermal effects and tool wear.
High-Speed Steel Tool Finishing
CBN abrasive wheels may be used in selected high-speed steel tool grinding applications. Confirm grit size, resin formulation, edge-quality targets and wheel conditioning.
Precision Mechanical Components
Evaluate appropriate resin-bond wheels for selected hardened shafts, precision components and other suitable ferrous workpieces where dimensional control matters.
Automotive Component Grinding
Selected hardened transmission or engine-related components may require precision grinding. Workpiece grade, wheel design, coolant and surface integrity must be assessed.
Resin-Bond CBN Wheel Manufacturing
CBN-B10 can be evaluated as the abrasive constituent of resin-bond grinding wheels where controlled grain fracture is part of the proposed tool design.
These are application-evaluation directions, not approved uses or performance guarantees. For lower-hardness steels, conventional abrasives may be more economical. For heavy-load grinding, higher-toughness CBN grades may be appropriate.
CBN-B10 vs. A10, A20 & B20 — Grade Comparison
SinoDiam’s four main CBN grit grades are differentiated by their catalogue-described crystal appearance, toughness positioning and intended abrasive-tool applications.
| CBN Grade | Crystal Positioning | Primary Application Direction |
|---|---|---|
| CBN-A10 | Amber · Irregular · Medium Toughness | Resin-bond grinding, grain-retention and controlled-fracture evaluation |
| CBN-A20 | Amber · Regular · High Toughness | Vitrified, metal and electroplated grinding tools |
| CBN-B10 | Black · Irregular · Friable · Low Toughness | Resin-bond fine grinding and potential cutting-edge renewal |
| CBN-B20 | Bright Black · Blocky · High Toughness | Selected higher-load grinding and multi-bond systems |
The table is a grade-selection framework, not an independently verified toughness ranking. Crystal color and appearance alone cannot establish abrasive quality, strength, purity or finished-wheel performance.
How to Select CBN-B10 for Resin-Bond Grinding Tools
CBN-B10 should be selected around the complete grinding process, including the desired relationship between abrasive grain fracture and finished-wheel wear.
Identify the Workpiece
Specify steel composition, hardness, heat treatment, geometry, removal requirements and surface-integrity targets.
Confirm the Resin-Bond System
Define the resin chemistry, fillers, curing process, abrasive concentration and wheel construction. Verify that the abrasive behavior matches the tool design.
Select Mesh & Friability
Choose an appropriate grit fraction and request the relevant particle-size distribution and friability information. Compare with CBN-A10 if required.
Validate Grinding Results
Evaluate grinding forces, wheel wear, grain loss, surface roughness, thermal damage and process economics under controlled testing conditions.
Should You Choose CBN-B10 or CBN-A10 for Resin Bond?
Both are positioned for resin-bond tools. A10 is an amber irregular CBN with medium-toughness catalogue positioning, whereas B10 is a black friable grade with lower-toughness positioning. A resin-bond wheel requiring greater grain integrity may favor one grade, while a process benefiting from controlled grain fracture may favor the other. Direct substitution should be established through matched trials.
SinoDiam CBN Grade Selection
Explore the four SinoDiam cubic boron nitride grades according to crystal characteristics, intended bond systems and grinding requirements.
Current Product
Current Grade · Black Friable
CBN-B10 — Friable CBN for Resin-Bond Grinding
Black, irregular and friable CBN abrasive positioned for resin-bond grinding systems where controlled grain fracture and cutting-edge renewal are important application considerations.
Primary selection focus: particle friability, resin-bond retention and precision grinding requirements.
Explore Other CBN Grades
CBN-A10 →
Medium-toughness amber irregular CBN positioned for selected resin-bond grinding tools.
CBN-A20 →
Relatively regular, higher-toughness amber CBN for selected vitrified, metal and electroplated tools.
CBN-B20 →
Blocky, higher-toughness black CBN for selected higher-load grinding and suitable multi-bond applications.
The existing CBN-B20 URL is /product/cnb-b20/. This link intentionally preserves the current address. A future slug correction should use an appropriate 301 redirect.
Frequently Asked Questions — CBN-B10
1. What is CBN-B10 Black Friable CBN?
CBN-B10 is SinoDiam’s black, friable cubic boron nitride abrasive positioned for selected resin-bond grinding tools. Its historical catalogue describes irregular particles with low-toughness grade positioning.
2. What does friable CBN mean?
Friable CBN describes abrasive grains that tend to fracture more readily under suitable mechanical conditions. The actual fracture response depends on particle properties, size, loading and bond retention.
3. Does CBN-B10 automatically self-sharpen?
No. Controlled fracture may expose additional cutting points, but excessive fracture or particle release can increase wheel wear. The resulting behavior must be evaluated in the finished tool.
4. Why is CBN-B10 primarily used in resin bonds?
Its friable grade positioning makes it a candidate for resin-bond grinding systems where the relationship between abrasive fracture and grain retention is important. Actual suitability depends on resin composition and wheel design.
5. Is CBN-B10 suitable for vitrified or metal-bond tools?
Resin bond is its primary catalogue application. Alternative bond systems require independent evaluation. CBN-A20 and B20 may be more appropriate starting points for selected vitrified, metal or electroplated tools.
6. What materials can CBN-B10 grind?
Potential workpieces include selected hardened tool steels, alloy steels, high-speed steel components and other suitable ferrous materials. Workpiece hardness, heat treatment and process conditions determine suitability.
7. Can CBN-B10 grind all carbon steels?
No. Different carbon steels vary in hardness and grinding requirements. Conventional abrasives may be more appropriate for some softer or less demanding workpieces. CBN selection should be justified by the actual process.
8. What mesh sizes are available for CBN-B10?
The historical SinoDiam catalogue references 50/60 through 325/400 mesh. Current fractions, grading standards, particle-size distributions and availability must be confirmed before ordering.
9. Is CBN-B10 suitable for fine grinding?
Fine grinding is a primary evaluation direction. Suitable results depend on grit size, wheel structure, dressing, workpiece material and other conditions. No fixed surface-quality outcome is guaranteed.
10. Does CBN-B10 guarantee Ra 0.8 µm or better?
No. Surface roughness is a result of the complete grinding operation. It depends on the finished wheel, abrasive size, dressing, workpiece, coolant and operating parameters.
11. Does CBN-B10 reduce wheel wear by 18%?
No universal wear-reduction percentage is established. Wheel life and abrasive consumption must be compared using a defined reference tool, matched workpiece and controlled test conditions.
12. What is the difference between CBN-B10 and CBN-A10?
CBN-B10 is described as black and friable with low-toughness positioning. CBN-A10 is amber and irregular with medium-toughness positioning. Both are primarily evaluated for resin-bond systems, but their grain-fracture behavior may differ.
13. What is the difference between CBN-B10 and CBN-B20?
CBN-B10 is friable and primarily positioned for resin-bond grinding. CBN-B20 is described as bright black, blocky and higher-toughness, with selected higher-load and multi-bond evaluation directions. Direct performance comparisons require appropriate testing.
14. Does black CBN color indicate higher purity or strength?
No. Crystal color is a visual product characteristic. Purity, toughness, friability and strength require appropriate testing rather than inference from color alone.
15. Does CBN-B10 prevent grinding burn?
No. Grinding burn depends on workpiece material, contact conditions, wheel sharpness, coolant, removal rate and machine parameters. A friable abrasive grade alone cannot guarantee protection against thermal damage.
16. Is CBN-B10 suitable for heavy-duty grinding?
High-load grinding may cause excessive fracture in a friable grain. More fracture-resistant grades may be appropriate, but the preferred abrasive should be selected through the actual grinding-tool requirements and tests.
17. Can CBN-B10 replace another supplier’s black CBN?
Not based on color and mesh size alone. Compare grading, crystal morphology, friability, toughness, bond compatibility and wheel-test results before making a substitution.
18. What information is required for a CBN-B10 quotation?
Provide the required mesh fraction, resin-bond formulation, wheel design, workpiece material and hardness, grinding conditions, trial requirements, estimated quantity and delivery destination.
SINODIAM INTERNATIONAL · CBN ABRASIVE TECHNICAL SUPPORT
Request CBN-B10 Black Friable CBN Specifications & Quotation
Looking for black, friable cubic boron nitride abrasive grit for resin-bond grinding wheels used on hardened steels, tool steels or other suitable ferrous components?
Share your required CBN mesh fraction, resin-bond formulation, finished-wheel design, workpiece material and hardness, grinding conditions, estimated order quantity and destination country.
SinoDiam can discuss the relevant CBN-B10 product specifications and the technical information needed to evaluate particle-size distribution, crystal friability, resin-bond compatibility and finished-wheel performance.