Product Overview
SinoDiam CBN-A10 Amber Irregular Cubic Boron Nitride is a synthetic CBN abrasive grit positioned for manufacturers of resin-bond grinding wheels and related precision grinding tools used on suitable ferrous materials.
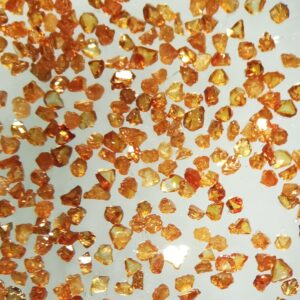
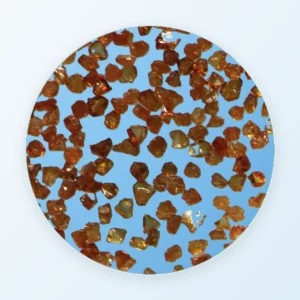
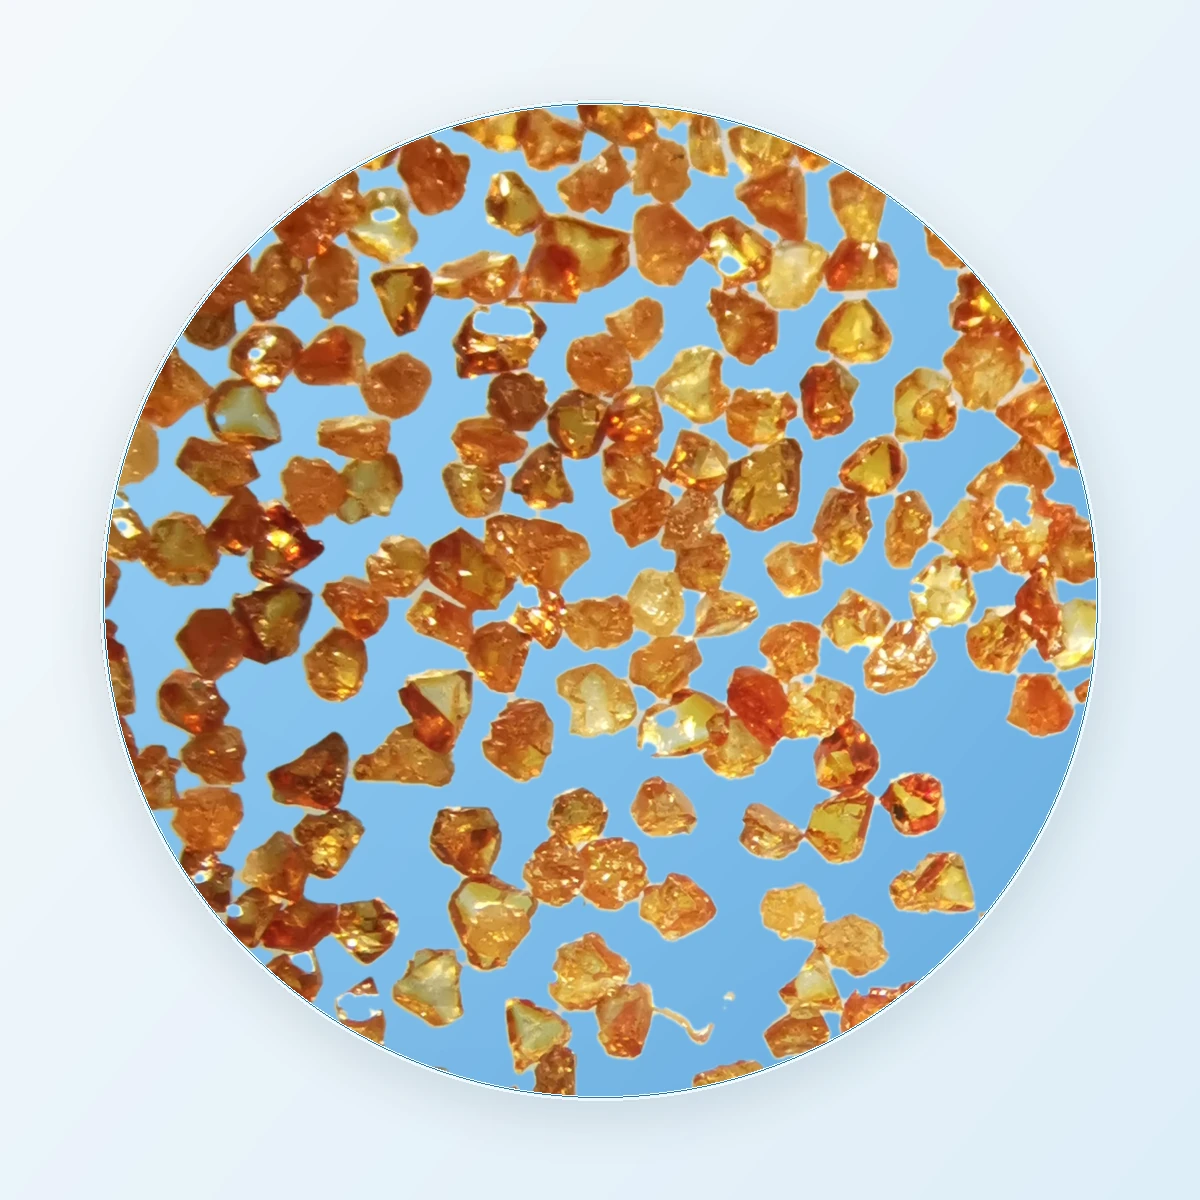
CBN-A10 is characterized in the SinoDiam product catalogue by an amber-colored, irregular crystal morphology and medium-toughness grade positioning. These characteristics make the material a candidate for resin-bond formulations where grain retention and controlled abrasive fracture need to be evaluated together.
Cubic boron nitride (CBN) is an important superabrasive for grinding many hardened steels and ferrous alloys. Compared with diamond, CBN generally offers more suitable chemical behavior in many steel-grinding applications. The preferred abrasive still depends on workpiece composition, heat treatment, temperature and grinding conditions.
In resin-bond grinding wheels, useful abrasive behavior requires a balance among crystal toughness, grain fracture, resin retention, abrasive exposure and bond wear. Irregular particles may provide multiple cutting contacts, but their shape alone does not guarantee improved adhesion or longer wheel life.
CBN-A10 can be evaluated for selected hardened tool steels, alloy steels, high-speed steel components and precision ferrous-metal grinding applications. The grinding load, heat treatment, wheel construction, coolant and required surface quality should be considered before selecting the abrasive grade.
The historical SinoDiam catalogue references 50/60 to 325/400 mesh CBN-A10 grit, with 50/60, 120/140 and 325/400 among the example fractions. Current particle-size availability, grading tolerances, crystal properties and applicable inspection data should be confirmed for each order.
CBN-A10 is primarily positioned for resin-bond applications. Vitrified, metal-bond and electroplated tool manufacturing may require different CBN crystal characteristics and should not be assumed compatible without separate qualification.
For technical selection, customers should provide the required mesh fraction, resin type, grinding wheel design, workpiece material, heat-treatment condition, grinding parameters and estimated quantity.
Technical Specifications
CBN-A10
Amber Irregular Cubic Boron Nitride
Synthetic Cubic Boron Nitride (CBN)
SinoDiam
Amber
Irregular
Medium — Catalogue Classification
Resin Bond
50/60–325/400 Mesh — Verify
50/60, 120/140, 325/400
Confirm Current Product Specification
Confirm Grading Standard and Limits
Request Grade-Specific Test Data
Confirm Representative Morphology
Selected Hardened Steels / Tool Steels
Suitable Alloy Steels / HSS Components
Resin-Bond CBN Grinding Wheels
Determine by Wheel Formulation
Application-Specific Validation
Determine by Grinding Process
Confirm Through Workpiece Trials
Request Applicable Product Data
The color, irregular morphology and medium-toughness positioning reflect the historical SinoDiam catalogue description. The available mesh fractions, measured toughness, PSD and performance values must be confirmed against current production specifications. No universal surface roughness, grit-shedding reduction, tool-life improvement or continuous grinding duration is guaranteed.
Amber Irregular CBN Crystal Morphology & Grinding Behavior
CBN abrasive behavior depends on grain morphology, internal crystal characteristics, bond retention and the mechanical and thermal conditions at the grinding interface.
Amber Irregular Crystals
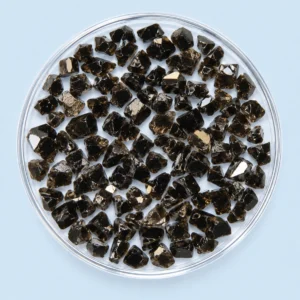
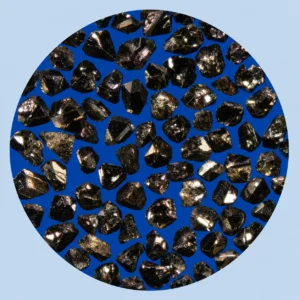
CBN-A10 is positioned as an amber-colored CBN grade with irregular particle geometry. Representative crystal images and actual grading should be reviewed for the ordered fraction.
Medium-Toughness Positioning
The catalogue describes A10 as a medium-toughness grade. Actual resistance to fracture depends on crystal quality, particle size and the measurement method used for qualification.
Potential Cutting-Edge Renewal
Under suitable conditions, controlled grain fracture may expose additional abrasive cutting edges. Excessive breakage can instead increase wheel wear or reduce grinding efficiency.
Grain Retention & Exposure
CBN must remain appropriately retained while worn grains and bond material are managed by the wheel structure. Resin chemistry, fillers, concentration and manufacturing conditions influence retention.
CBN–Workpiece Compatibility
CBN is widely selected for grinding hardened steels and other suitable ferrous alloys. Material hardness, alloy composition, heat treatment and grinding temperature affect the outcome.
Wheel Wear & Dressing Behavior
Wheel loading, glazing, grain pull-out, dressing and grinding conditions can alter cutting performance. CBN crystal selection must be integrated with the complete grinding wheel design.
What Does Self-Sharpening Mean for CBN?
Self-sharpening describes the renewal of effective cutting edges through suitable abrasive fracture and wheel wear mechanisms. It is not a permanent or automatic property of every CBN-A10 particle. The preferred degree of grain fracture depends on grinding load, workpiece properties and resin-bond retention.
Resin-Bond CBN Grinding Wheel Compatibility
CBN-A10 is primarily positioned for resin-bond abrasive tools. The grinding performance of a finished wheel cannot be determined from abrasive grain properties alone.
Phenolic Resin Systems
Selected phenolic resin grinding wheels may be evaluated with CBN-A10. Confirm resin grade, fillers, curing cycle, abrasive concentration and the wheel’s intended grinding conditions.
Polyimide Resin Systems
Polyimide-bond grinding tools may have different thermal and mechanical requirements. A10 compatibility should be determined through formulation and manufacturing trials.
Wheel Concentration & Porosity
Abrasive volume fraction, resin content, fillers and wheel porosity affect cutting forces, chip accommodation, coolant access and wheel wear. Select these parameters as part of the complete tool design.
Grain Retention & Bond Wear
Useful wheel behavior requires suitable particle retention while maintaining effective cutting-point exposure. Excessive grain release or glazing can reduce grinding performance.
Wheel Manufacturing Process
Pressing, curing, shaping and finishing conditions may affect abrasive distribution and bond performance. Actual manufacturing parameters must be matched to the chosen resin system.
Grinding & Dressing Trials
Evaluate cutting performance, wheel wear, surface quality, grinding forces and dressing requirements using representative workpieces and controlled operating conditions.
Resin bond is the primary catalogue application for CBN-A10. Compatibility with other bond systems is not established solely by the grade designation. For alternative bond requirements, evaluate CBN-A20 or CBN-B20 against the actual tool design.
CBN-A10 Mesh Size Selection for Resin-Bond Tools
The required CBN grit size depends on the grinding wheel, workpiece, stock-removal requirement and finished-surface target. The following three size fractions are taken from the historical product description and are shown as selection examples, not guaranteed current inventory.
50/60 Mesh
Coarser Grit Evaluation
Consider for suitable resin-bond grinding applications requiring relatively large abrasive particles. Confirm wheel geometry, grinding load and acceptable surface damage.
120/140 Mesh
Intermediate Grit Evaluation
Evaluate where intermediate abrasive size and a balance between material removal and surface requirements are relevant.
325/400 Mesh
Finer Grit Evaluation
Consider for selected finer grinding operations. Particle-size distribution, wheel bond and dressing conditions remain important to the final surface.
Important Mesh-Size Specifications
Grading Convention
Define the mesh-size standard and acceptance limits. Equivalent-looking grade names do not always indicate identical particle distributions between manufacturers.
Crystal Toughness by Size
Particle fracture behavior may vary with crystal size. Request appropriate grade-specific test information when toughness or friability is critical.
Oversize & Fines Control
Particle-size tails may influence surface defects, cutting behavior and abrasive distribution. Specify acceptable oversize and fine-particle limits where needed.
Finished-Wheel Performance
Grinding results depend on the abrasive fraction together with the resin matrix, wheel concentration, structure, coolant and operating conditions.
Historical Range vs. Current Availability
The earlier SinoDiam catalogue references 50/60 through 325/400 mesh CBN-A10. Customers should request the current available size list and relevant grading data before specifying the material for production.
Recommended Applications of CBN-A10
CBN-A10 may be evaluated for selected resin-bond grinding tools used on hardened ferrous materials. Application suitability depends on wheel formulation, workpiece hardness, heat treatment and machining conditions.
Hardened Tool Steel Grinding
Evaluate resin-bond CBN wheels for selected hardened tool steel components. Consider hardness, alloying elements, desired geometry, coolant and surface-integrity requirements.
Alloy Steel Precision Grinding
Selected alloy steel components may benefit from appropriately designed CBN abrasive tools. Crystal grade, bond and grinding parameters should be validated together.
High-Speed Steel Tool Finishing
CBN is an important abrasive option for suitable high-speed steel tools. Evaluate the required wheel grit, cutting forces, thermal conditions and edge-quality target.
Resin-Bond Tool Grinding Wheels
CBN-A10 can be evaluated as an abrasive constituent in resin-bond grinding wheels designed for compatible ferrous workpieces. The complete wheel formulation determines results.
Hardened Mechanical Components
Suitable hardened machine components may require controlled precision grinding. Assess workpiece condition, dimensional tolerance, surface finish and grinding burn risk.
Toolroom Grinding Applications
Selected toolroom grinding operations can be evaluated where resin-bond CBN wheels and appropriate dressing procedures are available.
These are application-evaluation directions rather than certified uses. CBN-A10 is not automatically suitable for every cast iron, stainless steel, carbon steel or hard alloy. Material state and actual grinding conditions must be considered.
CBN-A10 vs. A20, B10 & B20 — Grade Comparison
SinoDiam’s four CBN products differ in their catalogue-described crystal appearance, morphology, toughness positioning and intended abrasive-tool applications.
| Grade | Crystal Characteristics | Primary Evaluation Focus |
|---|---|---|
| CBN-A10 | Amber · Irregular · Medium Toughness Positioning | Selected resin-bond grinding tools |
| CBN-A20 | Amber · More Regular · Higher Toughness Positioning | Selected vitrified, metal and electroplated systems |
| CBN-B10 | Black · Friable · Lower Toughness Positioning | Resin-bond grinding with controlled grain-fracture evaluation |
| CBN-B20 | Bright Black · Blocky · Higher Toughness Positioning | Selected higher-load grinding and multi-bond applications |
These descriptions indicate catalogue positioning, not measured or universal toughness rankings. Black and amber color alone cannot establish CBN strength, purity or grinding performance. Confirm actual particle characteristics and grade-specific test data.
How to Select the Right CBN Abrasive for Grinding
Select the CBN abrasive according to the complete grinding application rather than choosing only by crystal color, nominal toughness or product code.
Identify the Workpiece
Specify the steel or alloy type, heat treatment, workpiece hardness, geometry and required dimensional or surface tolerances.
Define the Bond System
Determine whether the tool uses resin, vitrified, metal or electroplated bonding. CBN-A10 is primarily positioned for resin-bond tools.
Select Mesh & Crystal Behavior
Specify the required grit fraction, grain strength, fracture behavior, grinding load and desired abrasive retention characteristics.
Validate Finished-Wheel Results
Compare grinding forces, workpiece burn, surface quality, wheel wear, dressing behavior and process economics using controlled trials.
CBN or Diamond for Grinding Hardened Steel?
CBN is commonly preferred over diamond for many hardened ferrous-material grinding applications because of its chemical compatibility under relevant grinding conditions. Diamond remains an important choice for other materials, including many cemented carbides, ceramics and hard brittle workpieces. Select the abrasive based on the actual material and process rather than hardness alone.
SinoDiam CBN Grade Selection
Explore the four SinoDiam cubic boron nitride products and compare their intended grinding wheel applications.
Current Product
Current Grade · Amber Irregular
CBN-A10 — Resin-Bond CBN Abrasive
Amber-colored irregular CBN positioned for resin-bond grinding applications requiring evaluation of medium-toughness particle behavior, grain retention and controlled abrasive fracture.
Primary focus: Selected resin-bond grinding wheels for hardened ferrous workpieces.
Explore Other CBN Grades
CBN-A20 →
More regular amber CBN crystals positioned for selected vitrified, metal-bond and electroplated abrasive tools.
CBN-B10 →
Friable black CBN for selected resin-bond applications requiring evaluation of controlled abrasive grain fracture.
CBN-B20 →
Blocky black CBN positioned for evaluating higher-load grinding requirements and suitable vitrified, metal or plated bond systems.
The CBN-B20 product currently uses the existing URL path /product/cnb-b20/. Keep this link until any future URL correction is completed with an appropriate redirect.
Frequently Asked Questions — CBN-A10
1. What is CBN-A10 cubic boron nitride?
CBN-A10 is SinoDiam’s amber-colored, irregular crystal CBN abrasive positioned for selected resin-bond grinding wheel applications. Its catalogue toughness classification is medium, while current measurable properties should be confirmed by grade-specific data.
2. What does Amber Irregular CBN mean?
Amber describes the visual appearance of the abrasive crystals, while irregular describes their general morphology. Neither attribute alone guarantees purity, toughness, cutting ability or tool performance.
3. Why is CBN-A10 positioned for resin-bond grinding wheels?
Its catalogue-described morphology and toughness make it a candidate for resin-bond tools requiring a balance of retention and grain fracture. Actual compatibility depends on resin chemistry, fillers, manufacturing conditions and wheel design.
4. What materials can CBN-A10 grind?
Potential applications include selected hardened tool steels, alloy steels, high-speed steels and suitable ferrous components. Workpiece hardness, heat treatment, wheel structure, coolant and grinding conditions should be reviewed before selection.
5. Is CBN-A10 suitable for all carbon steels?
No. The suitability and economic advantage of CBN depend on material hardness, heat treatment, removal requirements and grinding conditions. Conventional abrasives may be preferable for some softer steels or less demanding operations.
6. What mesh sizes are available for CBN-A10?
Historical SinoDiam product information lists sizes from 50/60 through 325/400 mesh, including 50/60, 120/140 and 325/400 examples. The current available fractions, grading standard and size tolerances should be confirmed before ordering.
7. What is medium toughness in CBN-A10?
Medium toughness is the catalogue grade positioning. It does not establish a fixed fracture-strength value. Actual toughness and friability should be assessed using the relevant particle size and test method.
8. Does irregular CBN automatically improve resin adhesion?
No. Particle morphology may influence mechanical interaction, but resin adhesion and abrasive retention also depend on surface properties, resin composition, wheel concentration and manufacturing conditions.
9. Does CBN-A10 always self-sharpen during grinding?
No. New cutting points may form through controlled particle fracture under suitable conditions, but the result depends on grinding load, grain properties and bond wear. Excessive fracture can increase wheel wear.
10. Is CBN-A10 suitable for vitrified or metal bonds?
Resin bond is its primary catalogue application. Other bond systems require independent evaluation. SinoDiam CBN-A20 and CBN-B20 may be relevant alternatives for some vitrified, metal or electroplated applications.
11. What is the difference between CBN-A10 and CBN-B10?
CBN-A10 is described as an amber irregular grade with medium-toughness positioning. CBN-B10 is a black friable grade positioned for selected resin-bond applications requiring different grain-fracture behavior. Direct performance comparisons require matched testing.
12. What is the difference between CBN-A10 and CBN-A20?
CBN-A20 is described as having a more regular amber crystal morphology and a higher-toughness positioning, with broader vitrified, metal and electroplated bond evaluation directions. Grade substitution must be qualified for the actual tool formulation.
13. Does CBN-A10 guarantee Ra 1.6 μm or better?
No. Surface roughness is determined by the grinding wheel, grit size, dressing condition, workpiece, machine, coolant and operating parameters. A fixed Ra value cannot be guaranteed by the abrasive grade alone.
14. Does CBN-A10 increase grinding wheel life by 15%?
No universal improvement percentage is established here. Wheel life must be measured under defined comparative conditions using the actual resin-bond formulation, workpiece and grinding process.
15. Why choose CBN instead of diamond for hardened steel grinding?
CBN generally offers a more suitable chemical interaction with many ferrous alloys under relevant grinding conditions than diamond. The final selection still depends on the steel grade, heat treatment, process temperature and wheel construction.
16. What information is required for a CBN-A10 quotation?
Please provide the requested mesh fraction, resin formulation, intended grinding wheel type, workpiece material and hardness, grinding conditions, estimated order quantity and delivery destination. Existing CBN specifications or test results can support comparison.
SINODIAM INTERNATIONAL · CBN ABRASIVE TECHNICAL SUPPORT
Request CBN-A10 Amber Irregular CBN Specifications & Quotation
Looking for amber irregular cubic boron nitride grit for resin-bond grinding wheels used on hardened tool steels, alloy steels or other suitable ferrous components?
Share your required CBN mesh size, resin-bond formulation, wheel design, workpiece material, heat-treatment condition, grinding requirements, estimated quantity and delivery destination.
SinoDiam can discuss current CBN-A10 product specifications and the technical information needed to evaluate abrasive morphology, grain toughness, resin-bond compatibility and grinding performance.